A vapor line that looks perfect can still leak at a fitting nobody torqued, a gasket pinched in its groove or a probe seated half an inch short. Tightness testing is the step that converts visual confidence into measured certainty, and it deserves the same planning respect as the product line test it usually runs alongside. Handover without it is a promise, not a result.
What the test actually proves
A tightness test pressurizes the isolated vapor run and watches whether pressure holds over a defined period. It proves the connected system, every joint, seal and penetration between isolation points, behaves as one gas-tight envelope. It cannot prove which joint is leaking if the result fails, which is why sectioning the system into testable segments before backfill and before handover saves enormous diagnostic pain later.
Planning the test while the site is still open
| Planning item | Why it matters | Common miss |
|---|---|---|
| Test segments defined on the drawing | Failures localize to a segment, not the whole site | Testing everything as one lump |
| Isolation points agreed and available | Valves and caps must actually hold the boundary | A cap that cannot seat under pressure |
| Acceptance criteria written down | Everyone reads the same pass line | Arguing about drift after the fact |
| Stabilization time before readings | Temperature swings masquerade as leaks | Starting the clock immediately |
| Records tied to as-built locations | A passing number nobody can locate is worth little | Results logged without joint references |
Running the test without fooling yourself
The classic failure of a tightness test is not a leak but a false reading. Field discipline keeps the measurement honest:
- Close the segment, verify every isolation point and pressurize to the agreed level;
- Allow the stabilization period so air temperature settles before the gauge is read;
- Read and log pressure at fixed intervals with the same instrument throughout;
- If pressure drifts, check temperature and isolation before declaring a leak;
- Confirm a genuine failure by sectioning, then retest each half until the leak is bracketed.
Documenting the result for handover
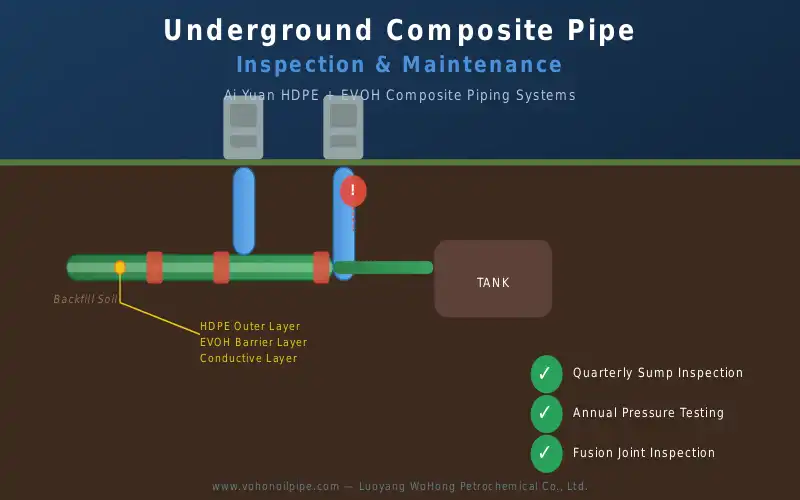
A test that passed but left no trace is a test that will be run again, at far higher cost, the first time a question arises. The handover record should carry the segment drawing, the acceptance criterion, the instrument used, the stabilization and observation times and the signed result. Composite vapor runs make this easy because their joints are numbered as installed, so each record maps cleanly onto the as-built.
Frequently asked questions
Should vapor lines be tested before or after backfill?
Before, wherever the schedule allows. A segment tested with joints exposed can be repaired and retested in minutes; the same failure found after backfill costs an excavation. Where phasing forces partial backfill, test every segment at the last moment its joints remain accessible.
Can a slow leak hide behind temperature change?
Yes, which is why stabilization matters more than the observation length. A warming day lifts pressure and can mask a small loss; a cooling afternoon fakes one. Stabilizing first and comparing against temperature movement separates real leaks from weather.
Who should witness the test?
Whoever signs the handover, plus the installing crew. A witnessed test transfers knowledge of the isolation layout and the record format, and it removes the later question of whether the numbers were produced the way the document claims.
Luoyang Wohong Petrochemical Equipment Co., Ltd. supplies double-wall composite fuel piping, fittings and electrofusion accessories for gas station and fuel depot projects. Contact us for pipeline layout review and product selection support.